|


|
|

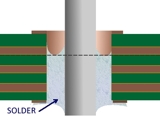
Problem Meeting Minimum Hole Fill During Wave Soldering
Board Talk
TranscriptPhil Comments
Jan 17, 2025
I've had these problems where there were no thermal reliefs for the vias connected to the ground planes. A design change solved the problem.
Scott W McKee, Golden West Technology
Apr 5, 2024
Everything that has been described is correct. If it is a thermodynamic problem, preheating is essential because it’s part of the demand on soldering heat. The higher the heat capacity of the PCB, the longer the preheating time required to achieve an even and homogeneous heat up. Medium-wave IR and convection heaters are advantageous. With high power short-wave IR heaters, there is a risk that the surface of the PCB will become too hot and the flux will already be consumed during preheating. The maximum allowable preheating temperature should be fully used, it depends on the flux type and the components.
We do not recommend top side temperatures higher than 130°C - 135°C. If the Elcap pins are made of alloy 42, they have a poor thermal conductivity. In this case, additional thermal vias in the pads of the thermal reliefs are helpful. They carry additional thermal energy to the top side of the PCB (during soldering) to achieve the required wetting temperature for solder fill. Top side heaters do not help in this case, as large Elcap’s shield the solder joints from the top side heat energy.
Juergen Friedrich, Ersa GmbH
Apr 3, 2024
Our past experience is that the use of an inert atmosphere, Nitrogen, significantly improves through wetting performance. The nitrogen will allow for the flux to stay active longer and promote improved wetting. N2 inerting retrofit kits are available to use with wave soldering systems.
Gregory K Arslanian, Air Products and Chemicals, Inc.
Oct 17, 2022
Gregory York, BLT Circuit Services Ltd
Feb 7, 2022
It could be your machine is not up to it. We had similar problem and it went away with a new 5 zone wave with jet fluxer.
Tim Swanson, Nemo Manufacturing Inc.
Jun 4, 2021
We have found in hundreds of experiments that the temperature of the solder in the pot correlates to hole fill. Try raising the temperature in 5 degree C increments.
Mitch Holtzer, Alpha Assembly Solutions
Aug 12, 2019
IPC Rev F mentioned clearly for the 50% solder fill acceptable, class 2 for the leads count more than 14. Earlier it was reflected as GND or PWR plane connection.
Dilipkumar Rathod, KES Systems and Services PTE Ltd
Jun 28, 2018
The alloy and flux type in use are significant variables that will impact hole fill. Some material sets can make life very difficult with high mass assemblies.
Timothy ONeill, AIM
Jun 28, 2018
Everything everyone said is true. I had a problem with a mixed technology aerospace board with all the components on the top. 16 heavy copper layers, the boards were 12 x 14 inches (board was originally designed in the 1970's). BIG electrolytics next to SMD parts (board revision was in the double digits). OA flux. We made sure that the components were solderable, The board had been properly cleaned, handled with clean gloves, and prebaked. The flux was sprayed on and the viscosity was in range. The immersion depth was correct, the angle was correct, Speed was correct. Requirement by print was 100% hole fill with a uniform solder fillet on top. DID NOT HAPPEN! The solder that did flow through was dull was grainy. We thought the problem was the automated setup for the heat and board speed. The top was not getting to the needed preheat and what was confusing was the not the electrolytics, but the inner layer ground and traces, away from the electrolytics was starving the preheat from sections of the board.
We tried adding multiple thermocouples on several runs. Cranked the preheaters up, slowed it down, started getting a wide difference in preheat from the thermocouples and we were concerned that we were on the edge of the degrading the boards, yet still no luck. It was the preheaters, they did not fail, just were degrading and inefficient, and the surface profiles on the heaters themselves showed that the heat varied greatly across them. Once upgraded, they did perform, and once we got a fairly uniform preheat of 525F across the top of the board (verified with thermocouples), the problem disappeared. A fully automated wave solder system is great when it works. Most of the time the adjustments work. But in the final analysis, the boards may just be too complex to fit in the profiles, so you have to go old school and use surface thermocouples. This issue probably cost us more than $350,000 in ruined boards, excessive rework, degraded performance, and a really nasty relationship with our customer, the prime. I hate to say it, but there really is an art (not an app) into producing legacy and mixed technology boards.
Joseph Fabian, Cetirus
Nov 15, 2017
Maybe you could check the wetting angle in the hole of capacitors with and without component and an other hole.
Imre Rácz, NIVELCO LTD
Jan 4, 2017
I've had those problems with components attached to the ground planes. A lack of a thermal relief has been the cause of most problems or thick boards. If I see that in the first article I then run a slower conveyor speed to get the board heated internally and give the solder a chance to wick up. Make sure your preheat tunnel sufficiently heats the top side of the board too.
Scott McKee, Golden West Technology
Dec 29, 2016
As per IPC-A-610 Rev. F, fill requirements for Class 2 & 3 are 75%. For class 1 it is not specified (table7-4). And the exemption of 50% for Class 2 connected to a thermal layer (7.3.5.1)has been removed in Rev. F
M. Davies, Excelitas
Dec 29, 2016
For the latest revision of IPC-610 (F), there is information that 50% of vertical fill is allowed only for components with 14 or more leads.
If want to be sure what is the possible root cause of vertical issue:
JJP, Fideltronik
Feb 11, 2016
Another design factor, beside the lead to hole ration, which you should reexamine is the thermal relief between the ground planes and the PTH holes. It is difficult to achieve the required hole fill if the hole does not have adequate thermal relief at the connection with ground and power planes.
Mike Rifahi, Avid
Feb 11, 2016
Inert atmospheres with nitrogen in the previous reflow oven process should help to decrease oxidation coming from that step. Correct nitrogen injection in the wave machine would also help to reduce metal parts oxidation and then improve wettability, resulting in better barrel filling.
Luiz Felipe Rodrigues, Air Liquide
Feb 10, 2016
One item not mentioned in the article is to ensure there is a proper venting path built into the capacitor. I have seen issue before where the capacitor is held tight against the PCB to prevent tipping and if the component does not have a venting path, pressure will build up under the component and force the solder out of the hole once the lead clears the wave.
Robert Babula, Continental Automotive
Feb 9, 2016
Another cause to consider is how flat does the Electrolytic Capacitor sit on top of the PCB. We have seen situations where the cap sits flush to the board and causes a back pressure that will prevent the solder from filling completely. If you can, you may consider holding the cap off the board to allow for the pressure release that will help the solder flow.
Mike Zurn, John Deere Electronic Solutions, Inc.
Apr 13, 2015
Ensure the drill inner walls completed platted. Try backing the board ( not OSP ) before wave process. If the board is OSP, try to complete the wave process as much as possible in two hours from prior SMT assembly process.
Parasu, Sanmina, India
Apr 1, 2015
Fill requirements per IPC are 75% for ALL three Classes. Not just Class 3. There is an exception for Class 1, 2 if connected to thermal or conductive layers acting as heat sinks.
Sheryl Payne, Controltek, USA
Apr 1, 2015
1. Pre-tin the cap leads. Minor cost adder, but best fix.
2. Brush tacky flux around the topside hole, including the cap leads. Tacky flux sticks around for the whole job and will immensely help promote hole fill. Be sure to match the formulation with the flux used in the machine. 3. Make sure the cap lead protrusion is between .030" to .060" if the assembly drawing allows it. Insufficient lead protrusion contributes to insufficient hole fill, solder voids, and lead contour not visible. Your touch-up operators could be removing solder to fix lead contour defects and be inadvertently giving you insufficient hole fill as a result.
R. Dean Stadem, Analog Technologies Corp, Lower Slobovia
Apr 1, 2015
Actually in IPC-A-610 Rev F which was released last summer, the only acceptable condition for less than 75% barrel fill, is when it's on a component with 14 leads or more. This is in regards to class 2 only, class 3 still has a minimum of 75% no matter the lead count.
Avery Armes, Adco Circuits, USA
|
||||||||


|
Free Newsletter Subscription
Circuitnet is built for professionals who bear the responsibility of looking ahead, imagining the future, and preparing for it. Insert Your Email Address |
|

|